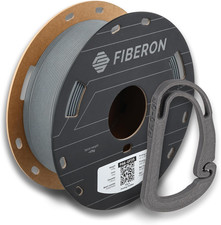
When you click on links to various merchants on this site and make a purchase, this can result in this site earning a commission. Affiliate programs and affiliations include, but are not limited to, the eBay Partner Network. Product description Fiberon PA6-GF25 3D printing filament HDT(°C) @0.45 MPa: 191 Bending modulus (dry-MPa): 4314 Bending modulus (wet-MPa): 1448 Material characteristics Reinforced with 25% glass fibers Print in Fiberon PA6-GF25 Comparison chart for Fiberon materials - Strong Nylon for Load-Bearing Parts: PA6-GF25 combines 25% glass fiber reinforcement with Nylon 6 to provide high strength, stiffness, impact durability, and layer adhesion for brackets, housings, jigs, fixtures, automotive components, and mechanical parts.
- Engineered Heat Performance: After annealing at 100°C for 16 hours, test specimens reach an HDT of 191°C at 0.45 MPa and 157°C at 1.8 MPa. These results are not continuous-use temperature ratings; actual performance depends on load, geometry, moisture, print orientation, and processing conditions.
- Keep Dry Before and During Printing: Nylon 6 absorbs moisture, which can reduce stiffness and strength while increasing flexibility. Store and print below 20% relative humidity. If exposed to moisture, dry at 100°C for 10 hours and print directly from a dry box when possible.
- Use an All-Metal Hotend and Hardened Nozzle: Print at 280–300°C with a 40–50°C build plate and the cooling fan off. Do not exceed the recommended bed temperature, as excessive heat may increase warping. A heated chamber is not required. Speeds up to 300mm/s are possible after calibration.
- Important Post-Printing Guidance: Anneal printed parts at 100°C for 16 hours when maximum thermal and mechanical performance is required. Remove same-material supports before the part absorbs excessive moisture, as the supports may become difficult to separate. Validate dimensions after annealing.
 |
|